Which visible glass-container feature must the inspection distinguish? Define acceptable, defective and marginal examples, including the pack variation and presentation on your line. A visible check does not replace hidden, functional or statutory tests.
Speak directly with Oxford Vision Systems about visible glass-container inspection.
Quick answer
Which visible defects can be detected on our glass containers?
Create a defect list with actual samples, distinguishing surface, shape, finish and foreign-material concerns. Identify the views available around the body, base and neck. Trial good and marginal examples under the proposed presentation, and document which requirements remain outside the demonstrated optical inspection scope.
Application decisions
Define what the camera can see on each glass container
Transparent, coloured and decorated glass need different optical trials. Divide the required checks by container region and inspection stage, then establish the coverage that can actually be demonstrated.
Decision 1
Separate body, base and finish checks
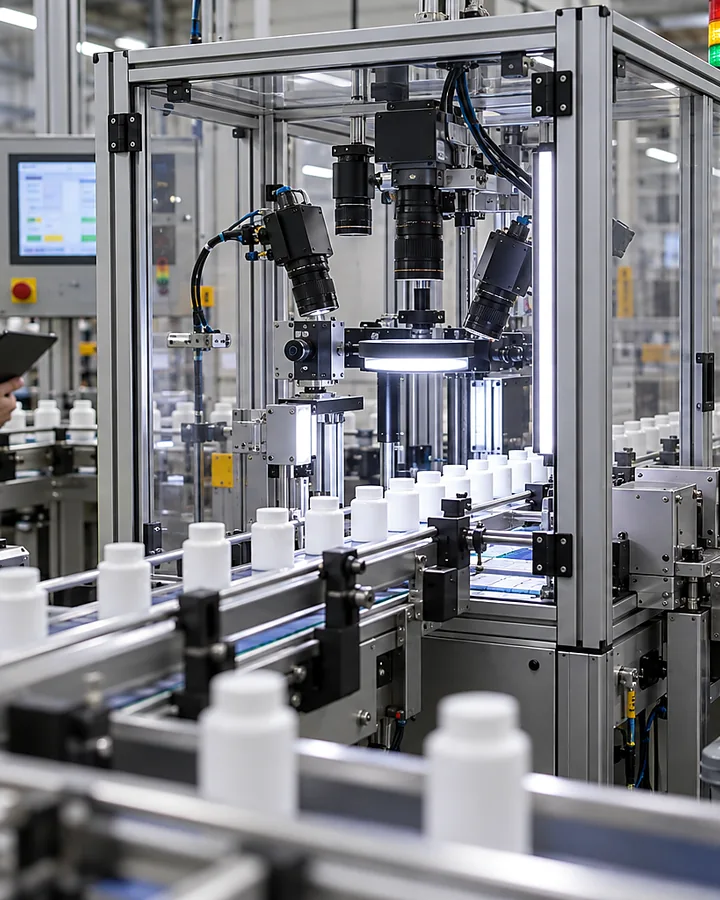
Mark the regions to inspect on a container drawing. The body wall, base and neck finish may need different views because features can obscure one another. List each visible defect with an example and an agreed decision. Do not describe a single side image as a complete container inspection when the opposite surface or base has not been examined.
Decision 2
Empty container or filled pack
State where the inspection sits relative to rinsing, filling, closing and labelling. Product, condensation, labels and closures can hide a feature that was visible earlier. If several stages need checking, identify them separately rather than expecting one camera station to answer every question. The proposed location should follow the visibility requirement and the line handling conditions.
Decision 3
Distinguish normal glass variation
Include acceptable mould seams, embossing, colour variation and surface appearance in the sample set. Compare these against the actual defects of concern so a system is not tuned only on unusually perfect bottles. Samples from different suppliers or moulds can be useful where they are approved for production. Keep the quality team’s accepted and rejected examples clearly identified.
Decision 4
Control the container presentation
Record orientation, spacing, wobble and any rotation at the inspection point. A useful optical trial reproduces these movements and the available viewing time. Review how lighting changes through curved walls and around the neck. A defect that is obvious while a sample is held still may be obscured when the container is moving or turned differently.
Decision 5
Track the result to the right pack
Identify the distance and transfers between inspection and rejection. Test missing triggers, uncertain results and a pack that stops or slips before the reject point. Confirm that the intended container is contained and that a failed reject produces the agreed line response. An inspection decision without reliable pack association cannot establish a controlled production result.
Decision 6
Document coverage and separate tests
Retain images and results for approved challenge samples by region and variant. List surfaces that remain hidden and defects not demonstrated in the trial. Visual assessment does not establish all strength, stress, sealing or product-safety properties of glass packaging. Those requirements remain with the responsible packaging and quality teams and their specified examination methods.
Two useful starting points for glass container inspection
The right choice changes with visible defect or measurement definition for visible glass-container inspection, good, bad and marginal sample range, your line layout and required results.
Your route from an initial enquiry to a working solution
You can review decisions about recipe, reject and line-control interfaces and false-accept, false-reject and challenge criteria at each stage.
01
Define the Visible Decision and Collect Representative Samples
Share representative good, bad and marginal samples, including the normal range for visible defect or measurement definition for visible glass-container inspection and the difficult good, bad and marginal sample range cases.
02
Prove Contrast, Presentation and Timing in an Optical Trial
Compare suitable methods and use focused trials to show how each option performs against part presentation and production speed.
03
Integrate Cameras, Controls, Reject Handling and Recipes
Connect the equipment to your line, services and controls while resolving optics, lighting and environmental conditions for day-to-day operation.
04
Challenge Marginal Cases and Document Agreed Results
Confirm recipe, reject and line-control interfaces, then complete and record false-accept, false-reject and challenge criteria before your operating team takes over.
Important limits
Know what needs a separate check
A camera can only assess a property made visible and repeatable by the inspection setup.
Sample diversity and marginal cases determine how meaningful a feasibility result is.
Visual inspection does not replace hidden, destructive, functional or statutory tests.
Your final solution for visible glass-container inspection must reflect the law, current standards and site-specific risks that apply to your installation.